Gehärteter Zahnradsatz — nach dem Härten geschliffen
Ein Satz Stirnräder und Antriebskomponenten, im weichen Zustand gefertigt, einsatzgehärtet auf 60 HRC und fertiggeschliffen, um den Härteverzug zu korrigieren.
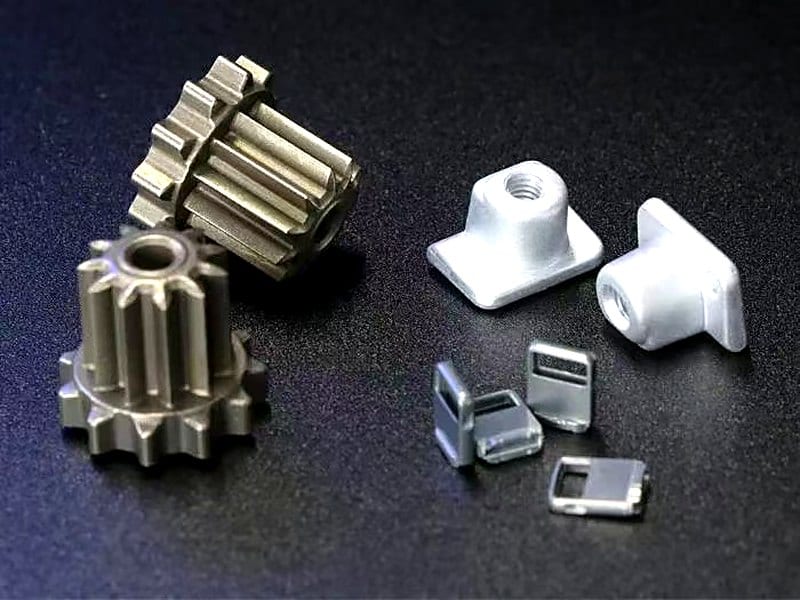
Bauteildaten
- Branche
- Industrial Machinery
- Verfahren
- Precision Grinding
- Werkstoff
- Steel 4140 / case-hardened
- Toleranz
- ±0.002 mm
- Oberfläche
- Ground, Ra 0.2 µm on flanks
- Stückzahl
- 400 / year
- Lieferzeit
- 25 working days
Kundendaten aufgrund eines NDA nicht genannt.
Herausforderung
The previous process hardened the gears after finish machining and accepted whatever distortion resulted. Noise levels varied between batches and roughly 12 % of parts fell outside the tooth profile tolerance after hardening.
Lösung
The routing was changed to machine in the annealed condition with a grinding allowance on the bore, faces and tooth flanks, then case-harden, then finish-grind. Bore and faces are ground on a cylindrical grinder; tooth flanks are profile-ground against the theoretical involute.
Ergebnis
Tooth profile now holds DIN quality 7 consistently. The out-of-tolerance rate after hardening fell from 12 % to zero, because the geometry is created after the distortion rather than before it. Measured noise at rated speed dropped by 4 dB(A).
Senden Sie uns noch heute Ihre Zeichnung
STEP, IGES, X_T, DWG, DXF, PDF oder STL. Jede Datei wird vertraulich behandelt und auf Wunsch durch ein NDA geschützt.