Juego de engranajes templados — rectificados tras el tratamiento térmico
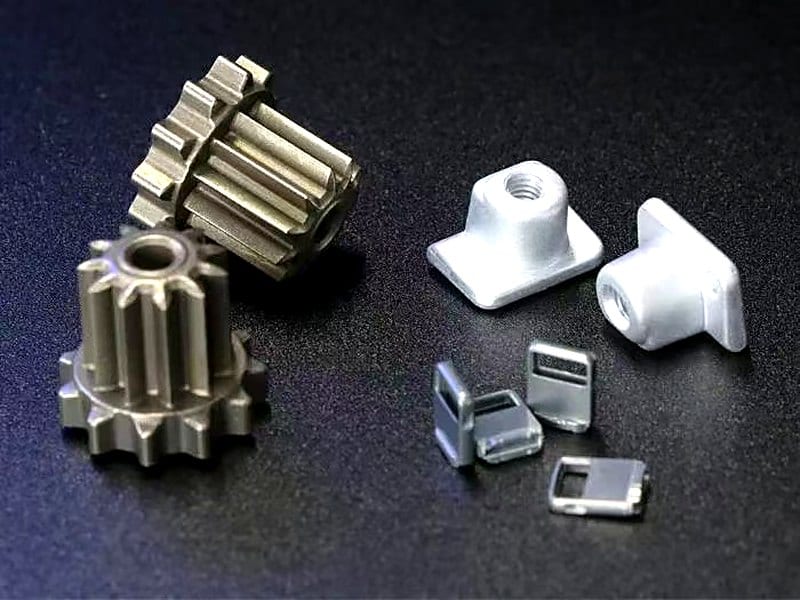
Un juego de engranajes rectos y componentes de transmisión, mecanizados en estado recocido, cementados a 60 HRC y rectificados para restituir la geometría perdida en el temple.
Especificación de la pieza
- Sector
- Industrial Machinery
- Proceso
- Precision Grinding
- Material
- Steel 4140 / case-hardened
- Tolerancia
- ±0.002 mm
- Acabado
- Ground, Ra 0.2 µm on flanks
- Cantidad
- 400 / year
- Plazo
- 25 working days
Datos del cliente no divulgados por NDA.
Reto
The previous process hardened the gears after finish machining and accepted whatever distortion resulted. Noise levels varied between batches and roughly 12 % of parts fell outside the tooth profile tolerance after hardening.
Solución
The routing was changed to machine in the annealed condition with a grinding allowance on the bore, faces and tooth flanks, then case-harden, then finish-grind. Bore and faces are ground on a cylindrical grinder; tooth flanks are profile-ground against the theoretical involute.
Resultado
Tooth profile now holds DIN quality 7 consistently. The out-of-tolerance rate after hardening fell from 12 % to zero, because the geometry is created after the distortion rather than before it. Measured noise at rated speed dropped by 4 dB(A).
Envíenos su plano hoy mismo
STEP, IGES, X_T, DWG, DXF, PDF o STL. Cada archivo se trata como confidencial y se cubre con NDA bajo petición.