Gestión de la calidad
Un sistema documentado, equipos calibrados y registros de inspección auditables.
Proceso de inspección
- 01
Incoming material
Lot logged, certificate verified, PMI where specified.
- 02
First article
Every ballooned characteristic measured and recorded.
- 03
In-process
SPC on nominated dimensions, on-machine probing.
- 04
Final inspection
CMM in a 20 ± 1 °C room, full report issued.
- 05
Packing & release
Protective packing, documentation pack, traceable label.
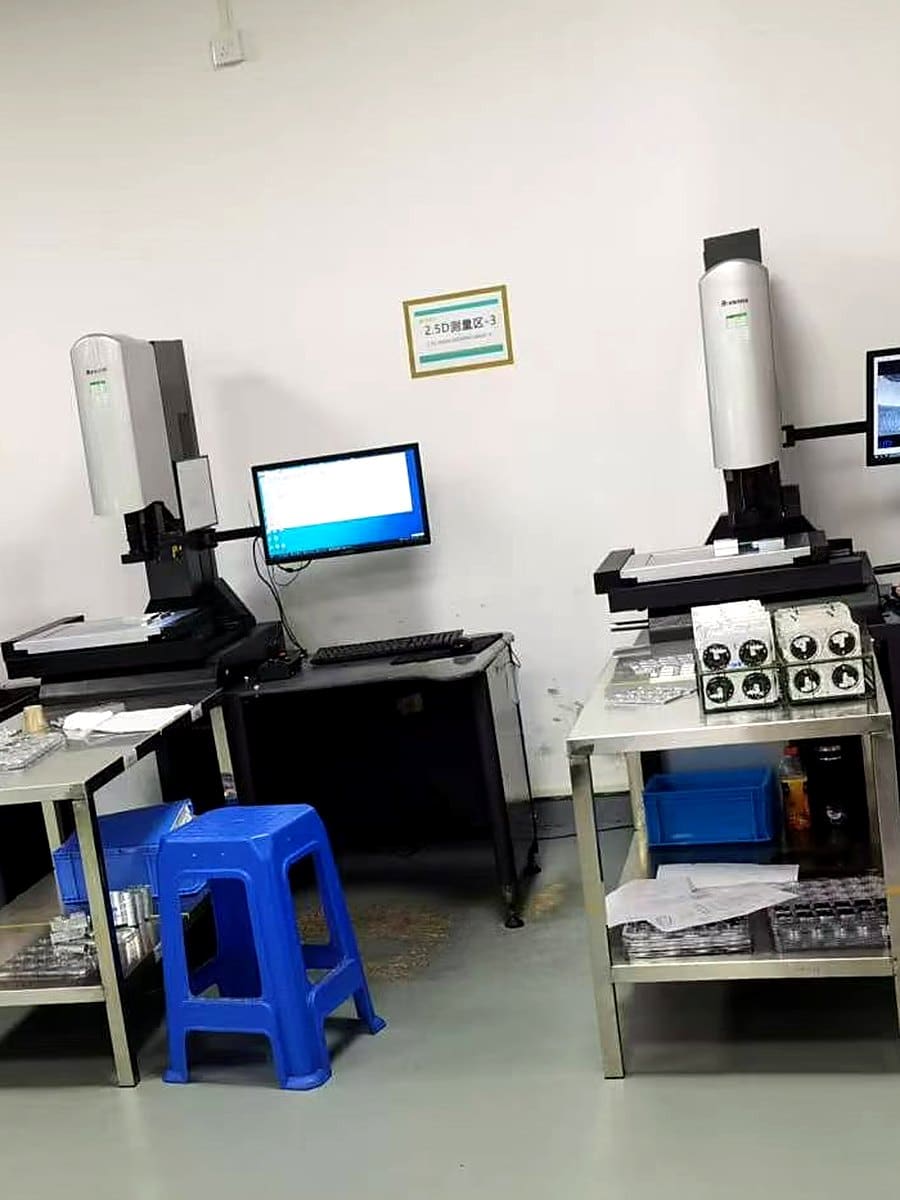
Temperature-controlled metrology room, 20 ± 1 °C.
Equipos de metrología
| Equipment | Capability | Qty |
|---|---|---|
| MMC de puente (sala climatizada) | 1000 × 800 × 600 mm, MPE 1.8 + L/350 µm | 3 |
| Sistemas de medición por visión | 400 × 300 mm, 0.001 mm resolution | 5 |
| Rugosímetros | Ra / Rz / Rt, 0.001 µm resolution | 4 |
| Medidores de altura y mármoles de granito | 600 mm, Grade 0 granite | 12 |
| Durómetros (Rockwell / Vickers) | HRC / HV / HB scales | 2 |
| Calibres de rosca y tampones | M1 – M64, UNC/UNF, BSP, NPT | 400 |
| Proyector de perfiles | Ø 400 mm screen, 10× – 100× | 2 |
| Medidor de espesor de recubrimiento (XRF) | 0.1 – 50 µm, multi-layer | 1 |
| Detector de fugas por helio | to 1 × 10⁻⁹ mbar·l/s | 1 |
| Banco de ensayo hidrostático | to 700 bar with chart recording | 1 |
Documentación que entregamos
Copias de los certificados disponibles bajo petición. Aceptamos auditorías de cliente e inspecciones de terceros (SGS, BV, TÜV).
La documentación técnica se mantiene en inglés para preservar la exactitud de los términos de ingeniería.
A quality system built for audits, not for marketing
Quality in contract machining is not a slogan — it is a set of records that survives scrutiny two years after the parts shipped. Our system is built around that test: every job carries a traceable chain from the purchase order to the raw material certificate, the machine, the operator, the programme revision, the inspection data and the packing list.
Incoming material control
Raw material arrives with an EN 10204 3.1 certificate and is logged against a unique lot number before it touches a machine. Lots are physically segregated and identified with colour-coded tags; the lot number follows the job travel sheet all the way to the packing list.
For medical, aerospace and pressure-service work, positive material identification (PMI) is performed on receipt and recorded.
First-article inspection
Before a production run is released, a first article is measured against every ballooned characteristic on the drawing. The report records the actual measured value and the measuring instrument used — not a pass/fail tick.
Where you work to AS9102, we issue Forms 1, 2 and 3 in the standard format. Where you work to PPAP, we supply the level (1 to 3) your programme requires, including control plan, process flow diagram, MSA and capability study.
In-process control
Nominated dimensions are monitored through the run at a frequency set by the control plan — typically first piece, every twentieth piece, and last piece for a 500-off batch. Where a characteristic is safety-critical or capability is marginal, the frequency increases and the data is plotted on an SPC chart.
Machine probes verify datums and critical bores on the machine before the part is released from the fixture, so drift is corrected while the part can still be saved.
Metrology environment
Final inspection is performed in a temperature-controlled room held at 20 ± 1 °C. Parts are allowed to stabilise before measurement — a 300 mm aluminium part measured at 26 °C reads roughly 0.03 mm larger than the same part at 20 °C, which is the entire tolerance band on a precision fit.
All measuring equipment is calibrated on a documented schedule against standards traceable to national reference standards, and the calibration certificate for any instrument used on your parts is available on request.
Non-conformance and corrective action
Non-conformances are recorded, contained, dispositioned and closed with a documented root cause. Where the escape reached a customer, we issue an 8D report with containment, root cause, corrective action and verification of effectiveness.
We do not argue about a tolerance we missed. If the part is outside the drawing, it is our problem to fix.
What you receive with every shipment
- Certificate of conformity referencing the drawing number and revision
- Dimensional report covering the critical characteristics
- Material certificate (EN 10204 3.1) on request or where the specification requires it
- Special process certificates — heat treatment, plating, passivation, NDT
- RoHS and REACH declarations where applicable
Calidad auditable
Inspección de primera pieza, SPC en proceso e informe dimensional en cada envío.