Eje de husillo inoxidable — torneado duro a Ra 0,2 µm
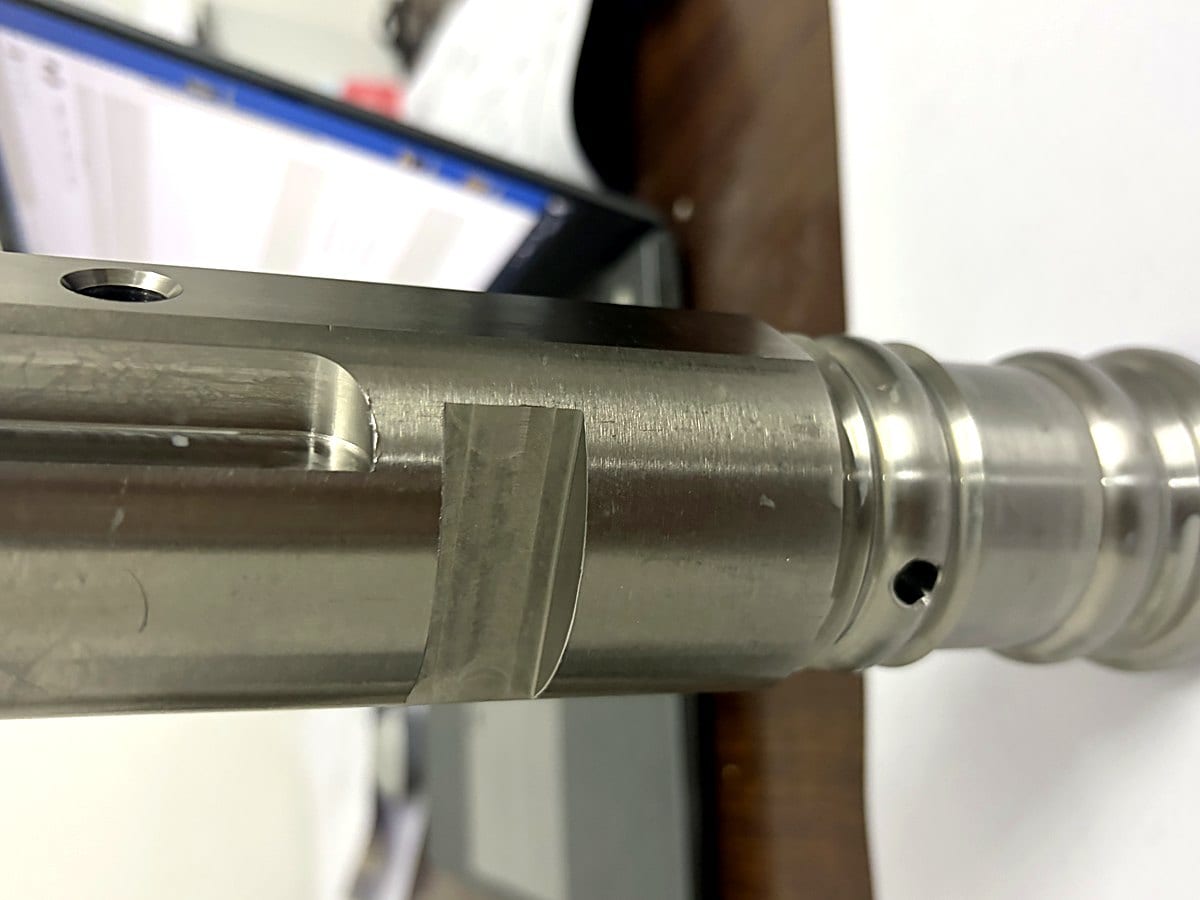
Un eje de husillo en 17-4PH torneado en duro en condición H900, alcanzando Ra 0,2 µm en el diámetro de sellado sin operación de rectificado.
Especificación de la pieza
- Sector
- Energy, Oil & Gas
- Proceso
- CNC Turning
- Material
- Stainless 17-4PH H900
- Tolerancia
- ±0.005 mm
- Acabado
- Superfinished, Ra 0.2 µm
- Cantidad
- 300 / year
- Plazo
- 19 working days
Datos del cliente no divulgados por NDA.
Reto
The shaft runs a lip seal at 6,000 rpm. The specification called for Ra 0.2 µm with no circumferential lay, which normally implies plunge grinding followed by superfinishing — two operations and a subcontract step.
Solución
We hard-turned the sealing diameter after age-hardening, using a CBN insert at high surface speed with a small nose radius and very low feed. A superfinishing belt pass removes the residual turning lay and brings the surface to a non-directional finish.
Resultado
Ra measures 0.16 – 0.19 µm with no measurable lay, meeting the seal manufacturer's requirement. The grinding subcontract was eliminated, cutting five days from the lead time and 21 % from the unit cost.
Envíenos su plano hoy mismo
STEP, IGES, X_T, DWG, DXF, PDF o STL. Cada archivo se trata como confidencial y se cubre con NDA bajo petición.